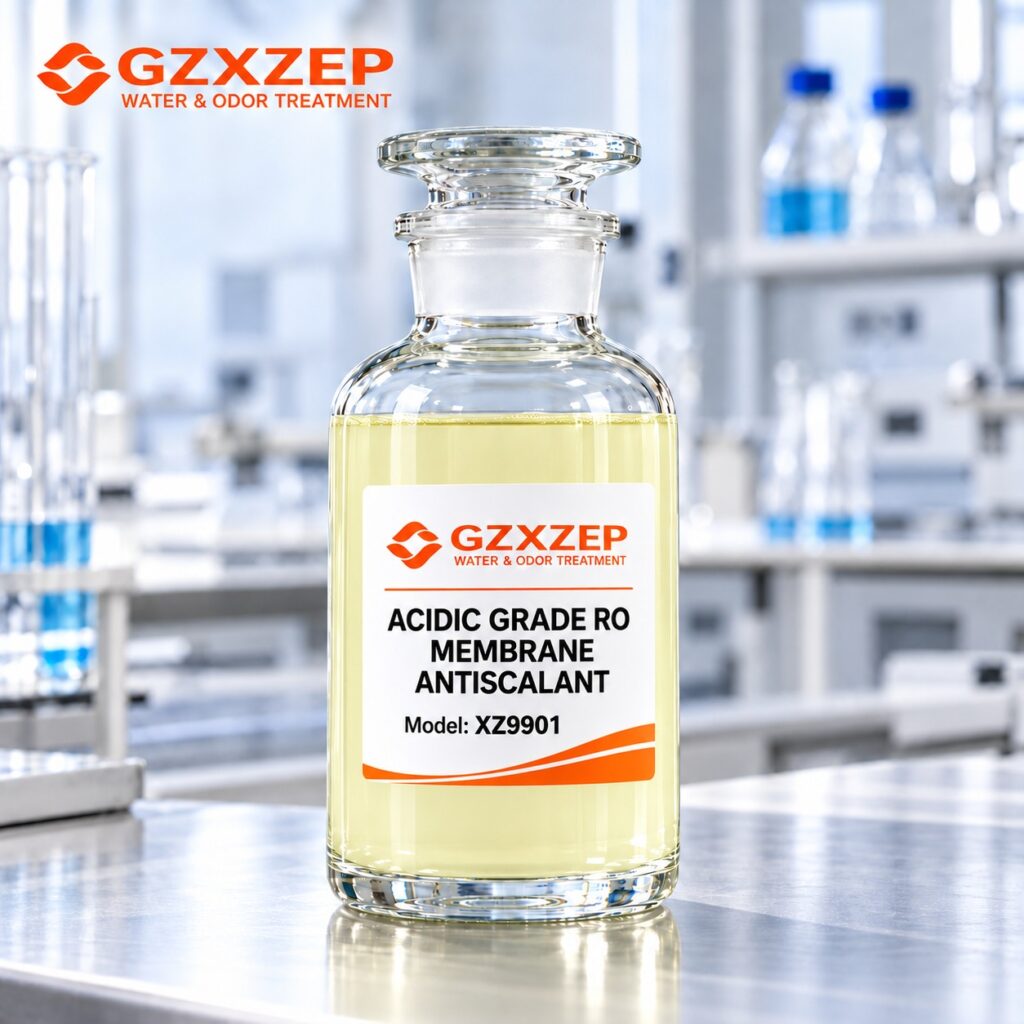
GZXZEP Acidic RO Membrane Antiscalant is a liquid scale inhibitor developed for reverse osmosis and nanofiltration feedwater. Its polymeric formulation interferes with mineral-crystal nucleation, growth and agglomeration, helping control carbonate and sulfate scale and maintain membrane flux and system recovery.
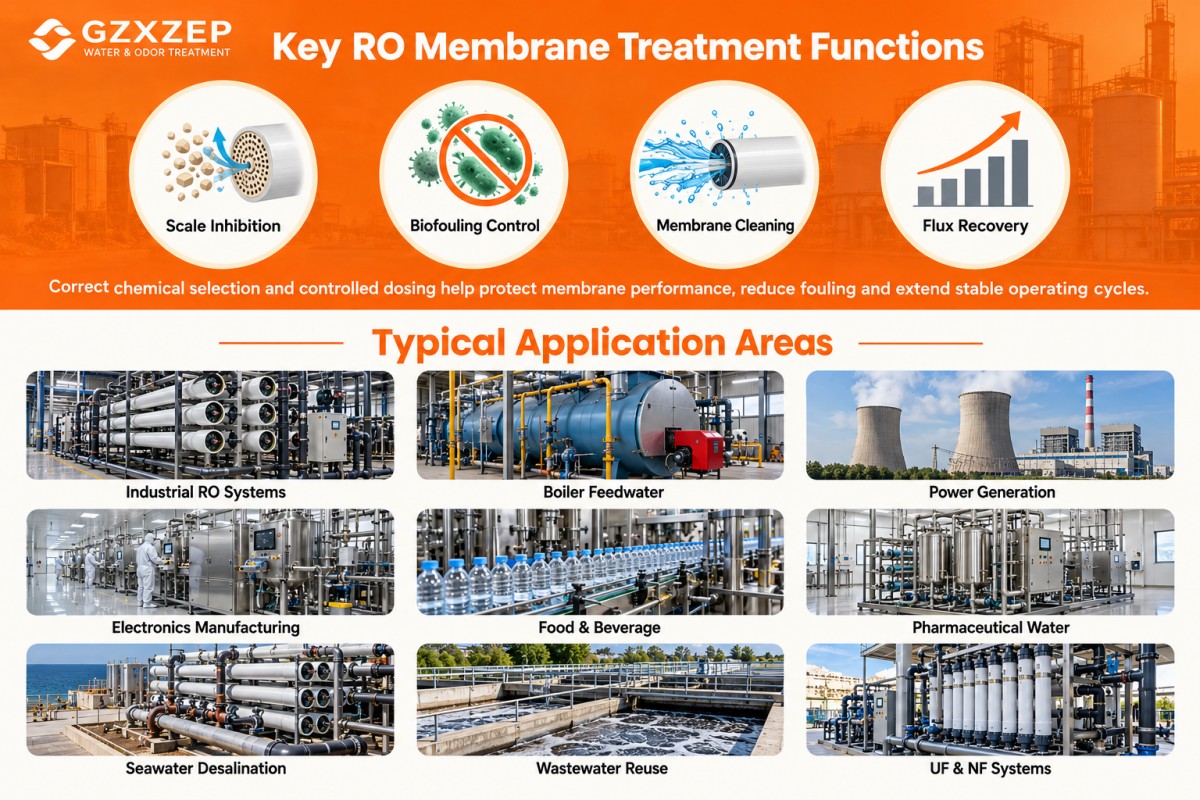
It is widely used in industrial RO and NF systems, brackish-water treatment, high-recovery membrane plants and feedwater with carbonate or sulfate scaling risk.
• Broad scale control over feedwater pH 5–9.
• Inhibits carbonate and sulfate crystal growth.
• Low reference dosage of 3–10 mg/L.
• Can be dosed neat or after approved dilution.
• Industrial RO and NF systems.
• Brackish-water treatment.
• High-recovery membrane systems.
• Feedwater with carbonate or sulfate scaling risk.
• Model: XZ9901.
• Appearance: Pale-yellow transparent liquid.
• pH: 2.5±0.5.
• Specific gravity: 1.10±0.05 g/cm³.
• Solid content: 33%.
• Reference dose: 3–10 mg/L.
• Minimum storage temperature: 0 °C.
1. The polymer adsorbs on early mineral crystals.
2. Crystal growth and agglomeration are inhibited.
3. Dispersed scale-forming salts remain in the concentrate stream and leave the system.
• Packaging: 25 kg drum or 1,000 kg IBC.
• Storage: Store sealed at room temperature in a dry and shaded place, away from direct sunlight and incompatible chemicals. Keep above 0 °C.
• Keep the container tightly closed after use.
• Customized formulation — The product and dose are selected from feedwater analysis, membrane type, recovery, pH and scale-projection results. This normally provides better treatment performance and overall cost efficiency than a one-formulation-for-all product.
• In-house manufacturing — Competitive factory pricing, stable batch quality and fast lead times.
• In-house laboratory — Rapid sample testing, formulation screening and continuous product improvement.
• Engineering support — Professional engineers provide product selection, dosing, commissioning and after-sales troubleshooting support.